

How to Choose the Motion Mechanism for High-Precision Dispensing Machines? 6 Key Transmission Selection Factors for Semiconductor and Precision Dispensing Equipment
Even with dispensing valve parameters adjusted to the extreme, why is the dispensed line width still inconsistent?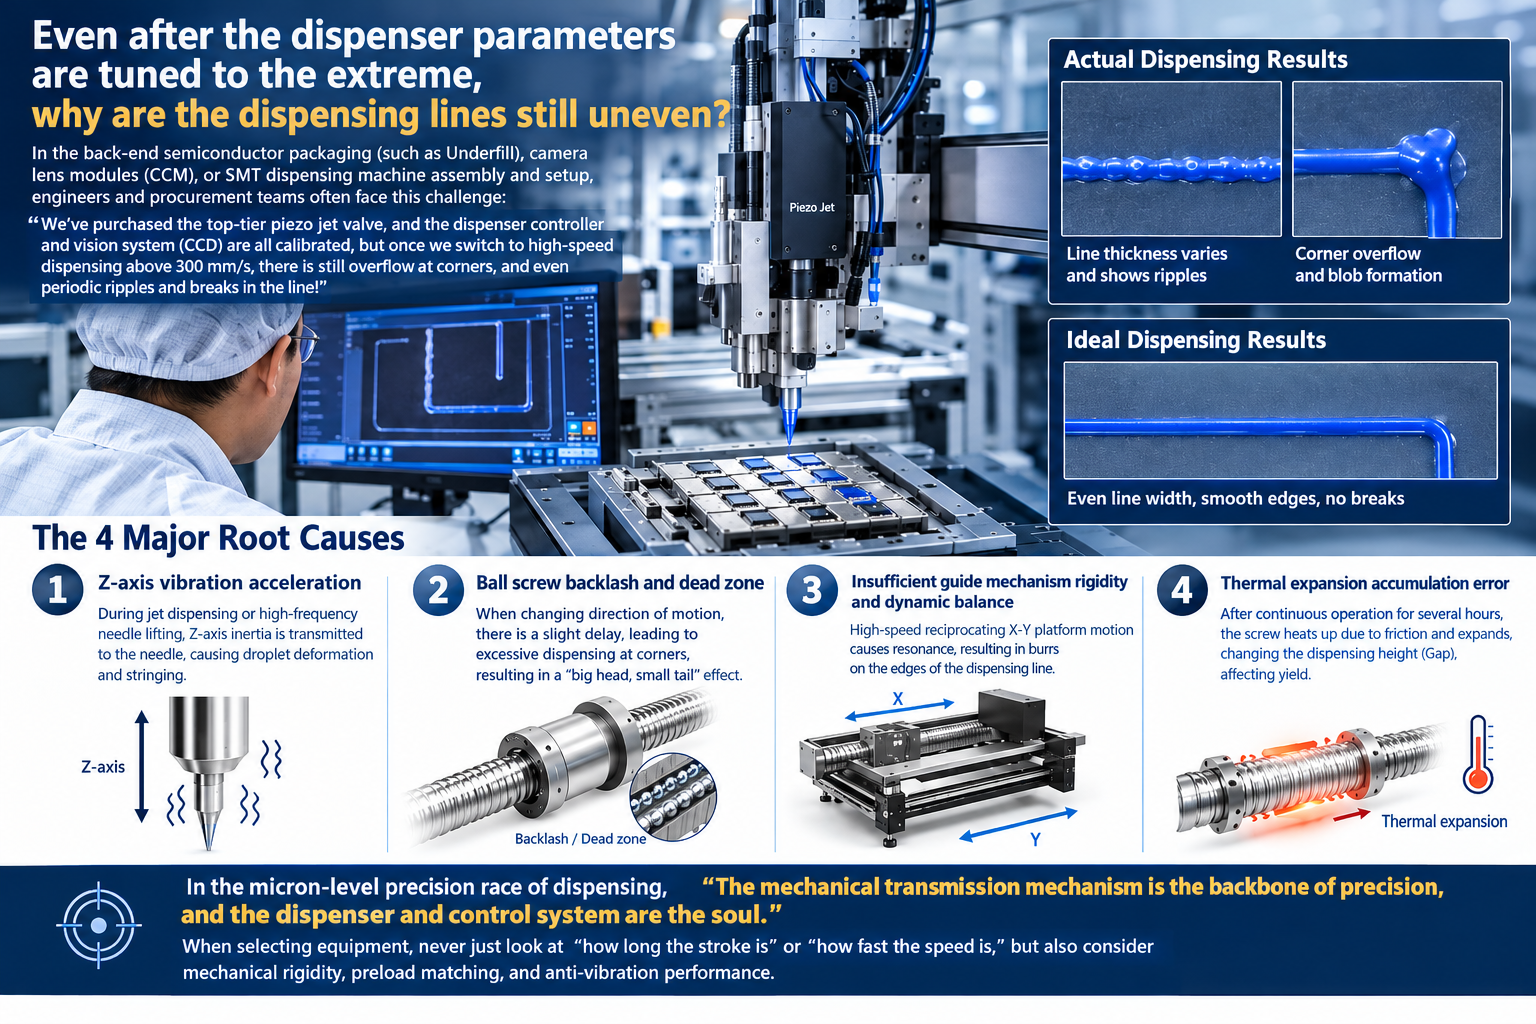
- Actual dispensing effect: Periodic ripples and broken lines in the straight segment, glue overflow at corners.
- Ideal dispensing effect: Uniform lines, no ripples, no glue overflow.
At the assembly and commissioning sites of semiconductor back-end packaging (such as Underfill), camera lens modules (CCM), or SMT dispensing machines, engineers and procurement professionals often encounter the following bottleneck:
"Even after purchasing top-tier piezoelectric jet valves, and calibrating the dispensing controller and vision positioning (CCD), glue overflow still occurs at corners once high-speed dispensing exceeds 300 mm/s, and straight segments are even accompanied by periodic ripples and broken lines?"
Many equipment development teams often attribute the problem to "unstable glue viscosity" or "insufficiently fast vision compensation," while ignoring the "micro-vibration" and "insufficient axial rigidity" of the mechanical motion transmission shafts:
- Frequent Z-axis acceleration and deceleration oscillation: During jet dispensing or high-frequency needle lifting, Z-axis inertial vibration is transmitted to the needle, causing glue dot deformation and stringing.
- Ball screw backlash and dead zone: A slight delay occurs when switching motion directions, leading to excessive glue dispensing at trajectory corners, forming a "fat head, thin tail" shape.
- Insufficient rigidity and dynamic balance of the guiding mechanism: High-speed reciprocating motion of the X-Y platform generates resonance, causing burrs on the edges of the dispensed lines.
- Thermal elongation cumulative error: After the equipment runs continuously for several hours, the screw expands due to frictional heat generation, changing the dispensing height (Gap) and affecting the yield rate.
In the competition for micro-level (μm) dispensing precision, "the mechanical transmission mechanism is the skeleton of precision, while the dispensing valve and control are just the soul." When selecting models, one must never only look at "how long the stroke is and how fast the rotation speed is," but must also examine mechanical rigidity, preload matching, and vibration resistance performance.
Master These 6 Key Factors First When Selecting Motion Mechanisms for High-Precision Dispensing Machines
|
Selection Criteria |
Key Questions to Confirm Before Design & Procurement |
|
Lead & Acceleration/Deceleration Matching |
High-speed dispensing (large lead) or micro-quantity dispensing (small lead)? Is the inertia ratio properly matched during acceleration and deceleration? |
|
Screw Accuracy & Preload Grade |
How should C3 / C5 ground accuracy grades be selected? Light preload or medium preload to balance service life and heat generation? |
|
Z-Axis Rigidity & Inertia Balance |
When the needle-lifting frequency reaches several tens of Hz, how can end-point micro-vibration of the cantilever module be avoided? |
|
Guide & Support Symmetry |
Does the coaxiality of the support assembly meet the required standard? Is the shaft rigidity sufficient to absorb frequent reversing impacts? |
|
Lubrication & Cleanroom Protection |
When the adhesive is sensitive to oil mist (e.g., in optical-component applications), how should the lubricant grade and dust-proof sealing be configured? |
|
Thermal Displacement Mitigation Design |
During continuous 24-hour operation, how can thermal expansion of a long-stroke axis be controlled to minimize its impact on positioning accuracy? |
- Lead and Resolution: The Choice Between High-Speed Jetting vs. Micro Line Dispensing
Depending on the dispensing process, dispensing machines have drastically different requirements for screw lead:
- High-speed surface jetting: The single-dot dispensing frequency is extremely high, and the X-Y axes require high-speed cruising and rapid stopping/starting. In this case, it is recommended to use a larger lead (e.g., 10mm or 20mm) to reduce vibration during high-speed motor operation and maintain operational smoothness.
- High-precision continuous trajectory gluing (e.g., wafer edge sealing, narrow bezel gluing): Requires extremely high resolution and stable low-speed constant velocity. Screws with a small lead (e.g., 1mm, 2mm, or 5mm) should be chosen to increase the motor equivalent reduction ratio and pulse resolution, avoiding trajectory jitter at corners.
II. C3 vs. C5 Grade Screws: Higher Precision Grade is Not Always Better
Procurement and mechanical design often intuitively assume that "dispensing machines must use C3 ground screw specifications," but in practice, a trade-off must be made among preload, temperature rise, and cost:
- Corner micro-stepping positioning (C3 grade + light/medium preload): In micro-level dispensing for semiconductor packaging, to eliminate axial play (Zero Backlash), appropriate preload must be applied to the screw. If excessive preload is selected, although rigidity is enhanced, frictional heat increases sharply during high-speed continuous motion, and the resulting thermal expansion counteracts the original precision.
III. Z-Axis "Micro-Vibration Suppression": The Secret to Overcoming High-Frequency Needle Lifting and Stringing
The most fatal and easily overlooked issue in dispensing machines is insufficient Z-axis rigidity:
- The dispensing valve body combined with sensors and heating jacket modules often weighs 1 to 3 kg, which is a typical cantilever load.
- When performing matrix dotting (Point-to-Point), the Z axis needs to reciprocate up and down several times to tens of times per second. If the clearance of the ordinary slider is slightly too large, micron-level residual vibration will be generated at the instant of startup and emergency stop, causing the glue droplet to move before it is completely severed, resulting in "trailing and stringing".
- Solution: The Z axis should adopt a high-rigidity dual-guide rail symmetrical configuration, or use needle roller guide set / preloaded micro linear guide bushings, providing excellent radial support rigidity to absorb instantaneous reverse impact forces, allowing the needle to stabilize within milliseconds after stopping.
IV. Coaxiality of Support Blocks and Fixed Ends: Eliminating Periodic Ripple Patterns
When the equipment applies glue along a straight line, if the glue line exhibits a "wavy" uneven thickness phenomenon, it is usually not due to unstable air pressure, but screw rotation runout:
- If the assembly concentricity of the screw fixed-side support unit and supported-side support unit is poor, rotation will force the screw to produce radial periodic runout.
- It is recommended to use an integrated precision support unit featuring high-coaxiality machining, and adopt an angular contact ball bearing preload configuration to absorb axial bidirectional thrust, ensuring that the runout during screw operation is strictly controlled.
V. Optical Anti-Pollution and Cleanroom Grade: The Invisible Test of Grease
In semiconductor cleanrooms or camera lens module (CCM) dispensing, minute volatiles can cause lens fogging or wafer surface contamination:
- Low-particle generation, low-volatility lubrication: Moving parts must be filled with cleanroom-dedicated fluorinated grease (PFPE) or high-grade low-dust lubricants to avoid generating tiny oil mists under high-speed friction.
- Surface corrosion-resistant treatment: If the dispensing process involves the volatilization of chemical solvents such as anaerobic adhesive, UV curing adhesive, or slightly acidic flux, it is recommended to apply electroless nickel plating or use stainless steel materials for guide rails and metal connectors to prevent surface rusting and seizure.
Motion Component Selection and Matching for Various Dispensing Equipment Types
|
Dispensing Equipment Type |
Typical Dispensing Requirements |
Recommended Screw / Guide Specifications |
Key Structural Design Considerations |
|
Semiconductor Post-Packaging Equipment (Underfill) |
High positioning accuracy (±3 μm), Class 100 cleanroom |
C3-grade ground ball screw (small lead 2–4 mm) + preloaded rigid support |
Oil-free lubrication management, low heat generation, dual-nut backlash elimination |
|
CCM Lens Module / VCM Dispensing Machine |
Micro-volume dispensing, Z-axis stable without vibration, miniature mechanisms |
Miniature ball screw (φ4–φ8) + precision guide bushing |
Reduce inertia, high-rigidity torsional resistance, eliminate reverse dead zones |
|
SMT High-Speed Circuit Board Dispensing Machine |
Long stroke, high-speed movement (>500 mm/s), high production efficiency |
High-lead ball screw (lead 10–20 mm) or belt + auxiliary guide shaft |
Lightweight slider, integrated suction-cup support structure, reduce track vibration |
|
Automotive Electronics / Thermal Management High-Flow Dispensing Machine |
Heavy load (large-torque dispensing valve), resistance to impact and vibration |
Large-diameter ball screw (φ15–φ20) + medium-preload guide rail |
Enhanced fixed-side bearing seat, reinforced dust protection, high-rigidity fixed support |
5 Parameters to Provide at Once When Inquiring for Mechanical Design and Equipment Procurement:
- Load weight and center-of-gravity cantilever length (total weight of dispensing valve, heating module, camera mechanism).
- Effective stroke and maximum operating speed/acceleration (e.g., X/Y stroke 400mm, acceleration 1.5G).
- Positioning accuracy and repeatability requirements (e.g., repeatability needs to reach specific microns).
- Working environment requirements (whether it is a cleanroom, whether there are chemical glue solvents volatilizing around).
- Fixing method and space constraints (shaft end machining type, motor direct-connected or side-mounted transmission).
Frequently Asked Questions (FAQ)
Q1: For glue overflow at dispensing corners, is adjusting software acceleration/deceleration or replacing the mechanism more effective?
Software acceleration/deceleration curves (S-Curve) can improve some vibration, but if the transmission mechanism itself has backlash or insufficient bearing rigidity, any emergency stop and turn will cause delay and mechanical elastic deformation. Only by selecting zero-backlash (eliminating play) precision preloaded screws and high-rigidity guiding mechanisms can the corner glue accumulation problem be fundamentally solved.
Q2: Does the Z axis of the dispensing machine need a transmission mechanism with a brake?
Highly recommended. Since high-precision dispensing machines mostly use vertical downward jetting, in the event of a sudden power outage, if the screw lead is large and lacks a self-locking function, the dispensing valve weighing several kilograms may drop due to gravity and directly crash into the workpiece or wafer. A transmission configuration with vertical anti-drop design, braking mechanism, or small-lead self-locking characteristics should be selected.
Q3: Can Handway provide customized shaft end machining for dispensing machine transmission modules?
Yes. In addition to standardized inventory specifications, for the compact mechanism space of equipment manufacturers, Handway provides precision ground machining of screw shaft ends, special outer diameter length customization, and overall tolerance matching services with motor couplings / bearing support units.
A stable and precise motion mechanism is the cornerstone of high-yield dispensing equipment. HANDWAY deeply cultivates high-precision mechanical components, providing ball screws, guide pillars/bushings, precision support units, and shaft series products, helping you build automated equipment with high speed, micron-level precision, and long life.
Footnote: What specifically is an "Integrated Precision Support Unit"?
In ball screw mechanisms, the traditional approach is usually to separately purchase a "Motor Bracket" and a "Fixed-side Support Unit," and then join them together with bolts during assembly. However, in micron-level equipment with high-frequency commutation and high-precision requirements like dispensing machines, using split combinations can easily produce slight axial angular deflection due to manual assembly tolerances or vibrations. Therefore, the industry often adopts the following two "integrated" designs:
- Motor Bracket Integrated Support Unit (Motor & Screw Integrated Unit)
- Structural Principle: Integrates the "servo/stepper motor mounting flange" and the "ball screw fixed side bearing housing" into the same metal body (single machined part).
Core Advantages: Completed within the same CNC machining process for the motor mounting pilot and bearing bore, completely eliminating joint surface gaps and cumulative tolerances between split parts, giving the motor shaft, coupling, and screw axis extremely high coaxiality, and greatly reducing runout during rotation.
- High-Rigidity Integrated Fixed-Side Support Unit
- Structural Principle: Adopts an integral rigid cast iron / steel unit, with factory-matched preloaded ultra-precision Angular Contact Ball Bearings (back-to-back DF/DB configuration) assembled inside.
- Core Advantages: Can withstand powerful bidirectional axial impact forces during high-speed reciprocation of the dispensing head, and prevents runout caused by micro-deformation of the housing under stress.
Main Functions (Addressing Dispensing Machine Pain Points)
- Eliminating Screw Runout: Prevents the screw from generating periodic wave-like vibrations like a jump rope during rotation, preventing uneven thickness ripples in the dispensed glue line.
- Reducing Mechanism Length and Weight: Eliminates redundant connection flanges and bolts, making it especially suitable for the compact mechanism space of dispensing machine X-Y axes.


