- Home
- Products
- Food Waste Bin
- Commercial Food Waste Bin (with Dedicated Strainer Basket)
Product List
Product Description
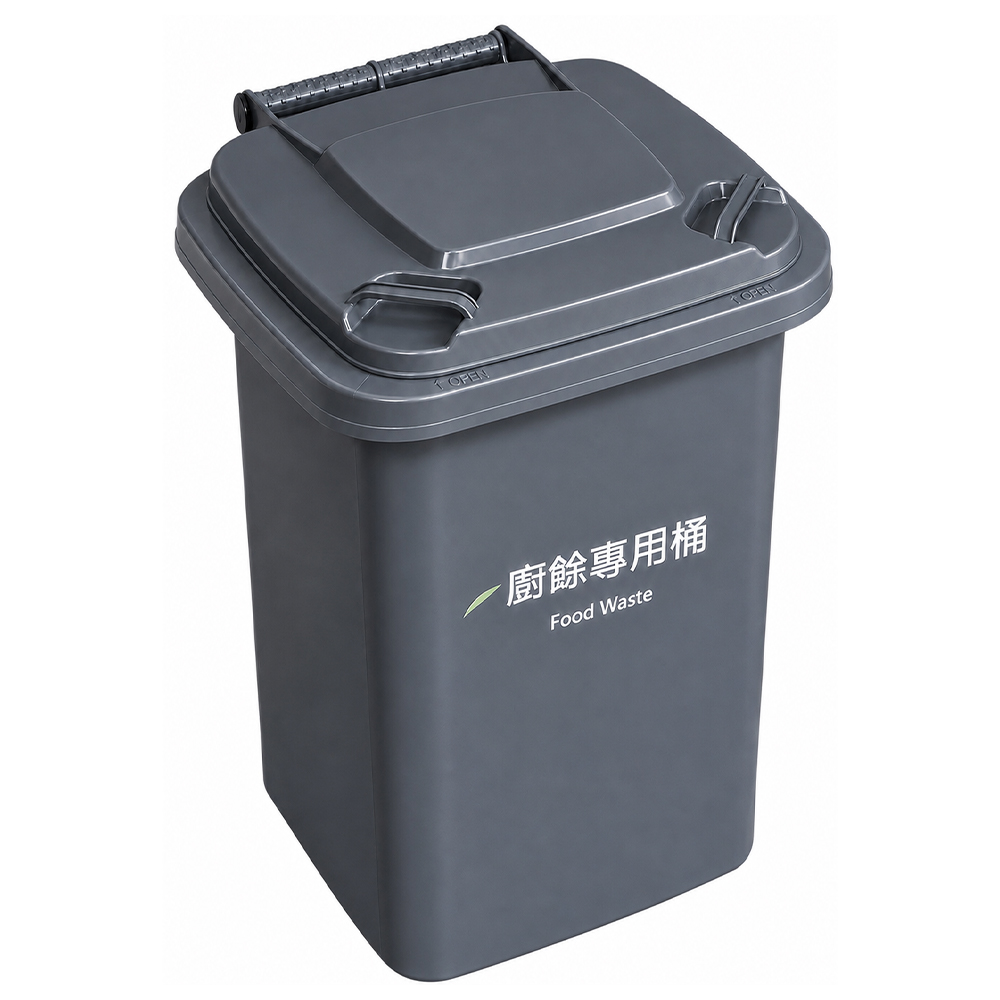
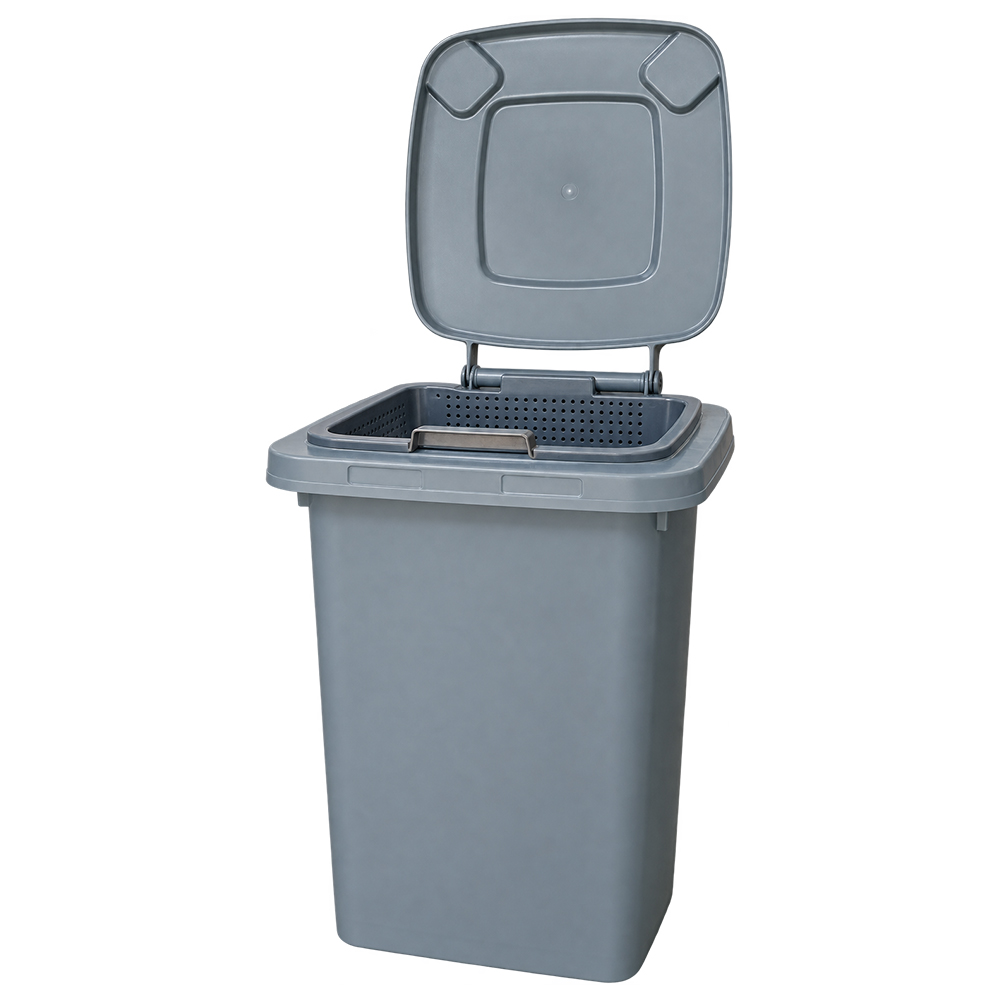
Solid-Liquid Separation • Efficient Collection • Odor Control & Hygiene — Tailored Food Waste Pre-Treatment Solution for Commercial Kitchens & StorefrontsEngineered specifically to solve food waste pre-treatment challenges in convenience stores, restaurant chains, hotels, cafes, and commercial kitchens: The 50L high-capacity outer bin paired with a dedicated 15L strainer basket achieves rapid solid-liquid separation. A tight-sealing lid effectively contains odors and prevents pest infestation, while ergonomic handles ensure effortless lifting and emptying. Seamlessly compatible with commercial food waste processors, it significantly reduces kitchen maintenance workload and maintains high standards of hygiene.
Download
- Product Specification
- Product Characteristics
- Why you must choose HEADWAY
| Item | Specification |
|---|---|
| Product Name | Commercial Food Waste Bin (with Dedicated Strainer Basket) |
| Product Type | Commercial Grade (Ideal for convenience stores, restaurant chains, beverage shops, cafes, dessert shops, central kitchens, etc.) |
| Outer Bin Capacity | 50 Liters (50L) |
| Strainer Basket Capacity | 15 Liters (15L) |
| Material | High-Density Impact-Resistant Engineering PP (Acid & alkali resistant, oil-repellent, scratch-resistant, and easy to clean) |
| Structural Design | Independent solid-liquid strainer basket, wide-angle sealed flip lid, ergonomic non-slip carrying handle, dual side-lifting handles on the inner basket |
| Color & Finish | Matte Dark Gray (stain-resistant finish) |
| Compatibility | Usable standalone as a dedicated commercial kitchen food waste bin, or paired as a pre-treatment unit for commercial food waste processors |
- High-Efficiency Solid-Liquid Separation: Built-in 15L Strainer Basket Reduces Downstream Processing Load
- The dedicated inner strainer basket features dense, evenly distributed drainage perforations along the bottom and sides, enabling immediate separation of liquid runoff from solid food waste.
- Significantly reduces moisture content to slow down odor-causing fermentation, while directly enhancing the drying and grinding efficiency of downstream waste processors—shortening processing time and reducing energy consumption.
- 50L Optimal Commercial Capacity: Meets Peak Volume Demands While Saving Floor Space
- Tailored for high-paced foodservice workflows, the generous capacity easily accommodates heavy food waste during peak dining hours, reducing the frequency of bag replacements and waste disposal runs.
- The sleek, slim, vertical profile minimizes floor footprint, fitting neatly beside dishwashing sinks, in kitchen aisles, or waste disposal corners without obstructing crucial workflow routes.
- Airtight Odor-Sealing Lid: Comprehensive Odor Containment for Superior Hygiene Standards
- The tight-sealing lid fits securely to the bin body, effectively trapping fermentation odors and preventing fruit flies, cockroaches, and other pests from gathering.
- The wide-opening flip lid ensures smooth, mess-free disposal, supporting effortless single-handed operation to boost front-line staff efficiency.
- Ergonomic & Hands-Free Handling: Clean Pouring and Simplified Maintenance
- Equipped with a sturdy, wide rear handle for stable and effortless transport; the inner basket features dual ergonomic side handles for clean, hands-free lifting, draining, and emptying.
- Smooth, rounded interior corners prevent grease and grime accumulation, allowing quick cleaning with water and neutral detergents to minimize routine maintenance effort.
- Industrial-Grade Durability: Acid, Alkali, and Heavy-Load Resistant
- Constructed entirely from heavy-duty impact-resistant PP, offering exceptional resistance to acids, alkalis, and oils to prevent cracking, embrittlement, or leakage under frequent commercial use.
- The modern matte dark gray finish resists stains and wear while providing a clean, professional aesthetic that blends seamlessly into any commercial kitchen or store environment.
- The Ideal Companion for Reduction Systems: Closed-Loop Green Workflow
- Serves as the dedicated front-end companion for Commercial Food Waste Processors, performing instant solid-liquid separation right at the collection stage.
- Streamlines the entire cycle: Collection → Rapid Draining → Smart Volume Reduction, empowering businesses to build cleaner kitchens and achieve ESG sustainability goals.
HEADWAY presents you with superior quality, firm commitment, and a spirit of partnership. As a manufacturer of automation and mold components, we possess deep knowledge of automation and mold technology, continuously innovating and improving to ensure outstanding performance and reliability.
On the official HEADWAY website, you can not only browse product catalogs but also understand that each product represents our commitment to quality and our responsiveness to customer needs. We rigorously control the manufacturing process, utilizing high-quality materials and precision machining to ensure that every product meets your expectations.
- Streamlined Production
- No minimum order quantity, we can produce even one.
- 100% inspection - From production to inspection equipment, all steps are completed by HEADWAY.
- Accept custom processing inquiries based on provided drawings.
- For product issues and subsequent after-sales service, we provide personalized assistance for you.